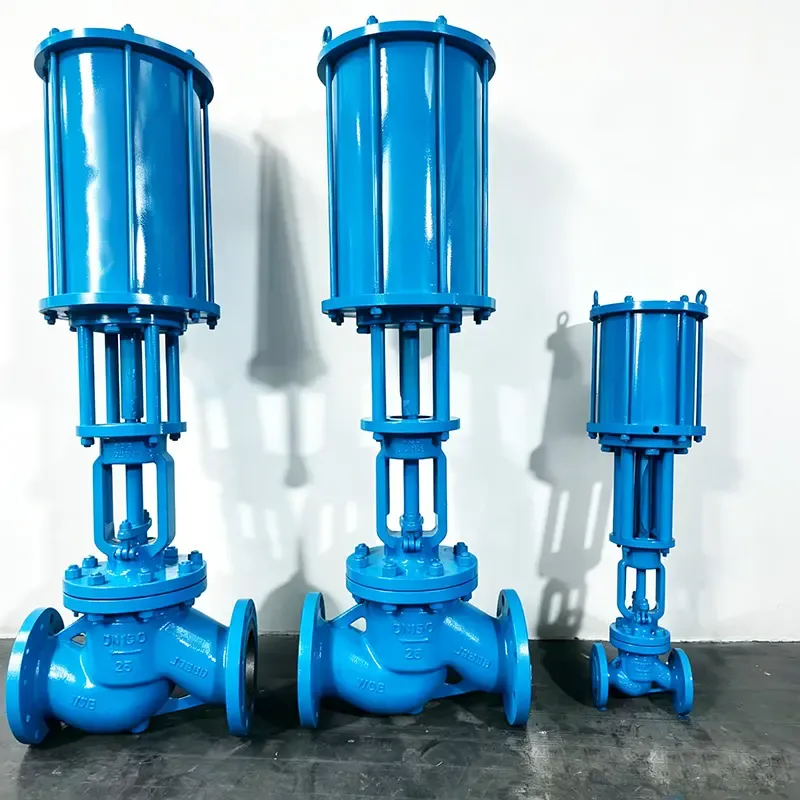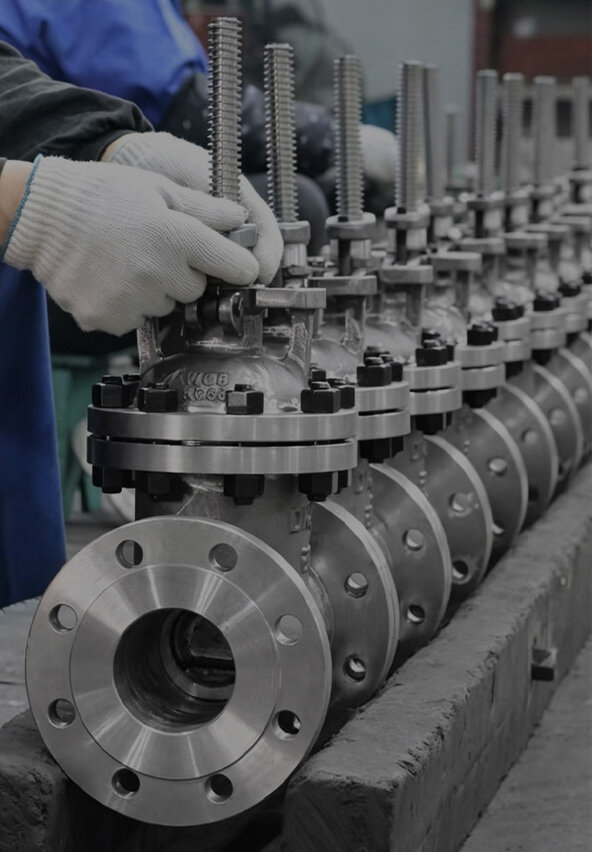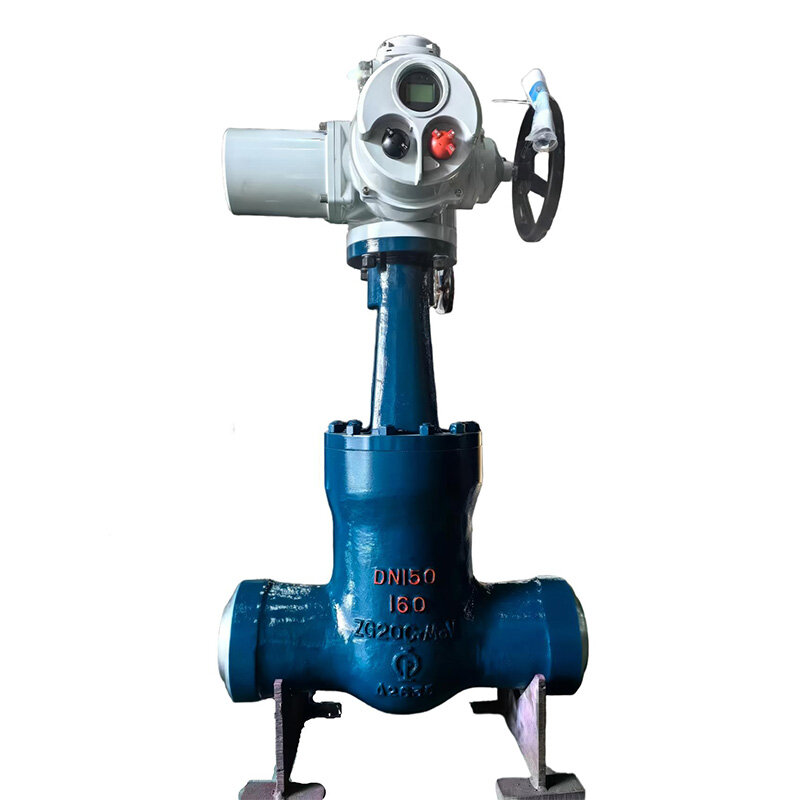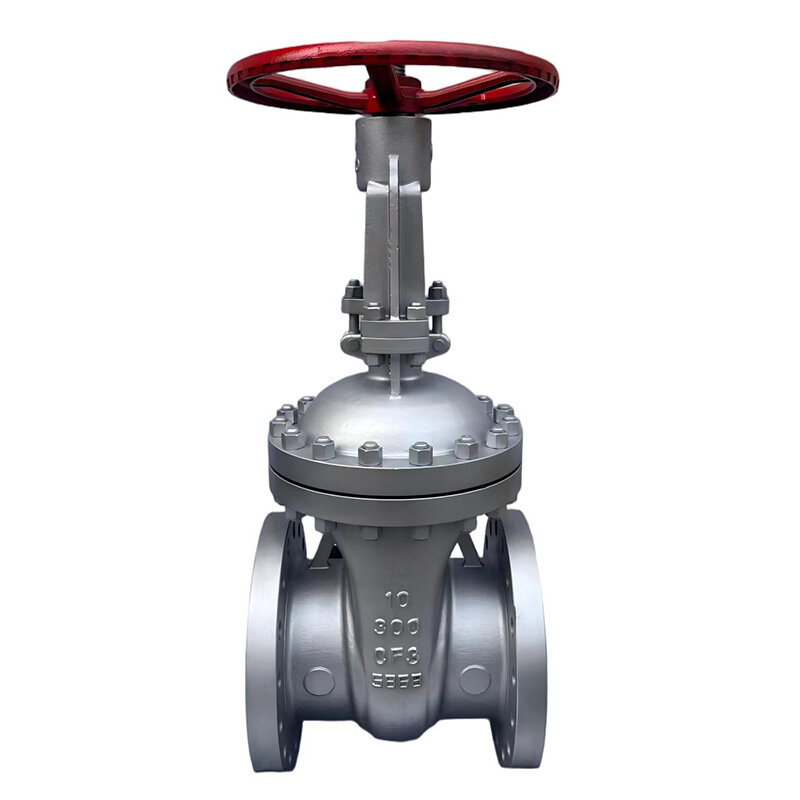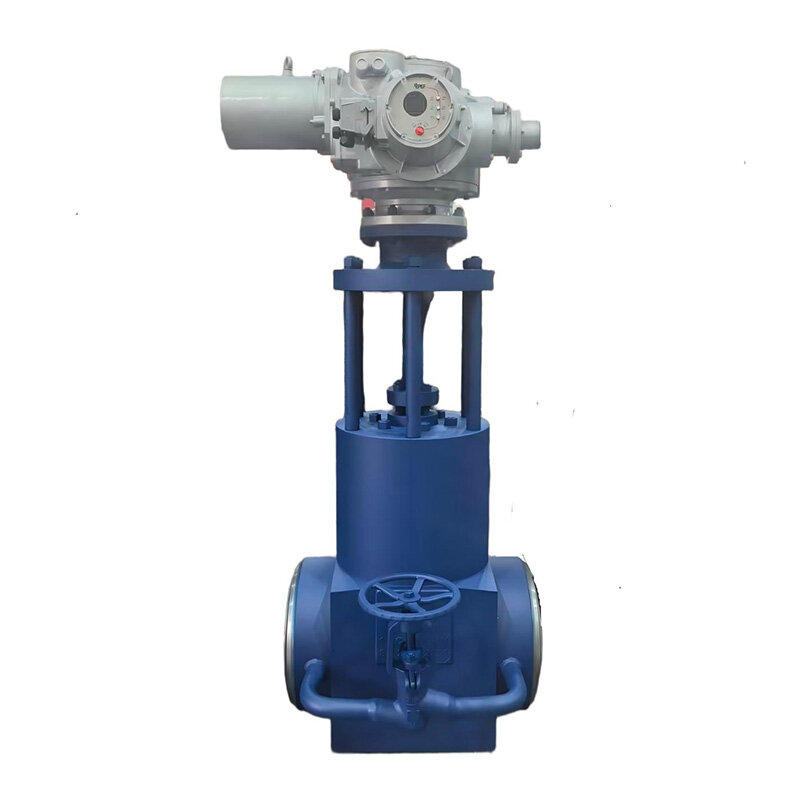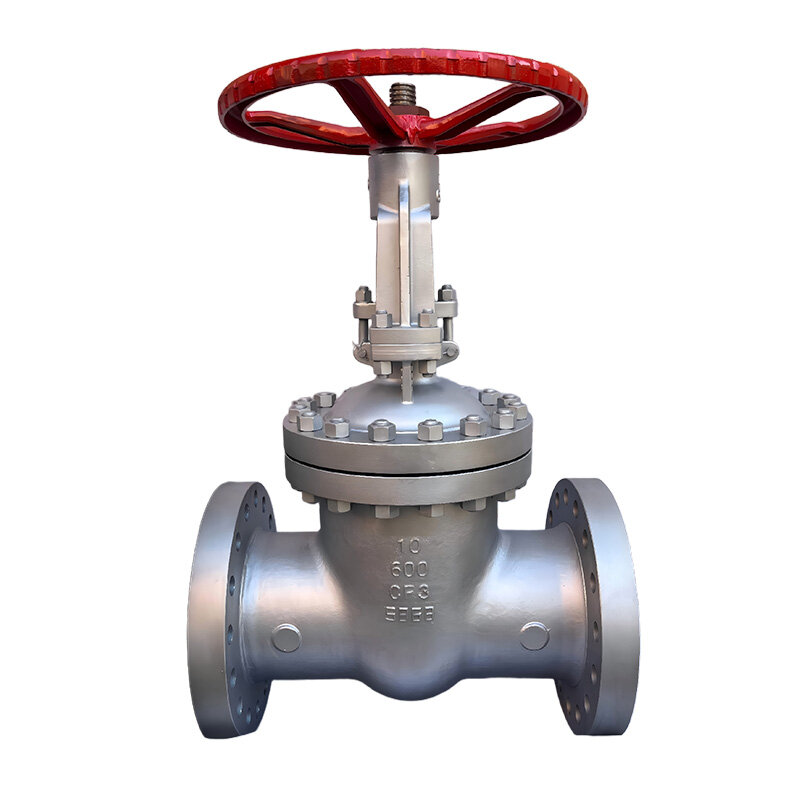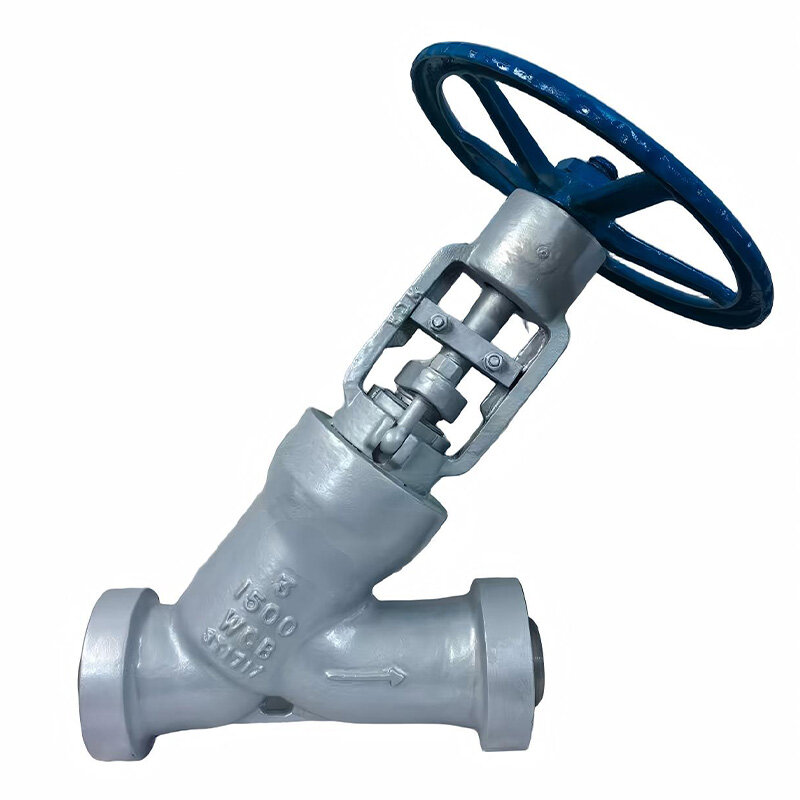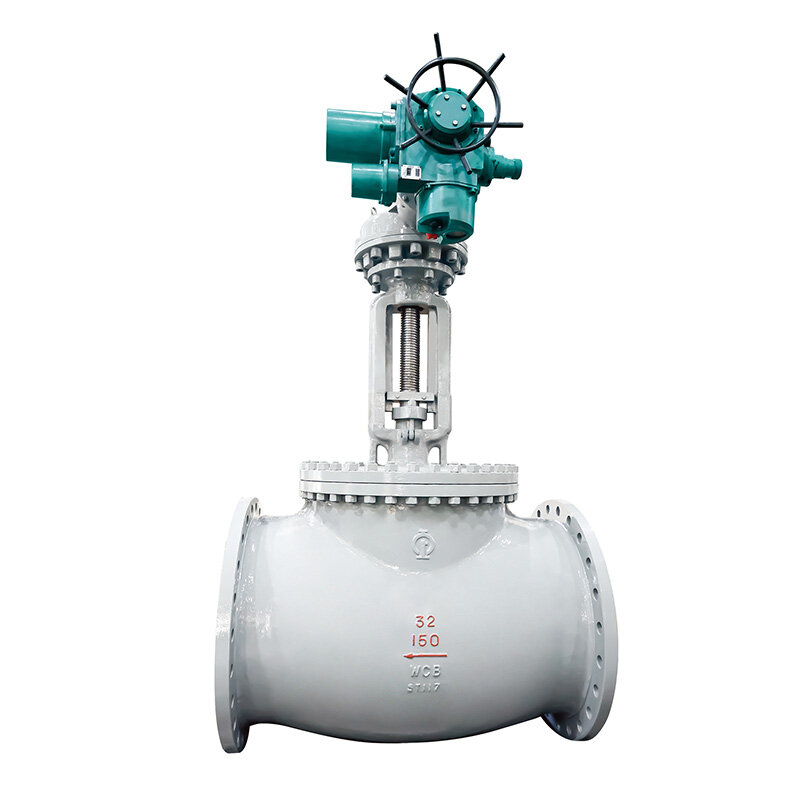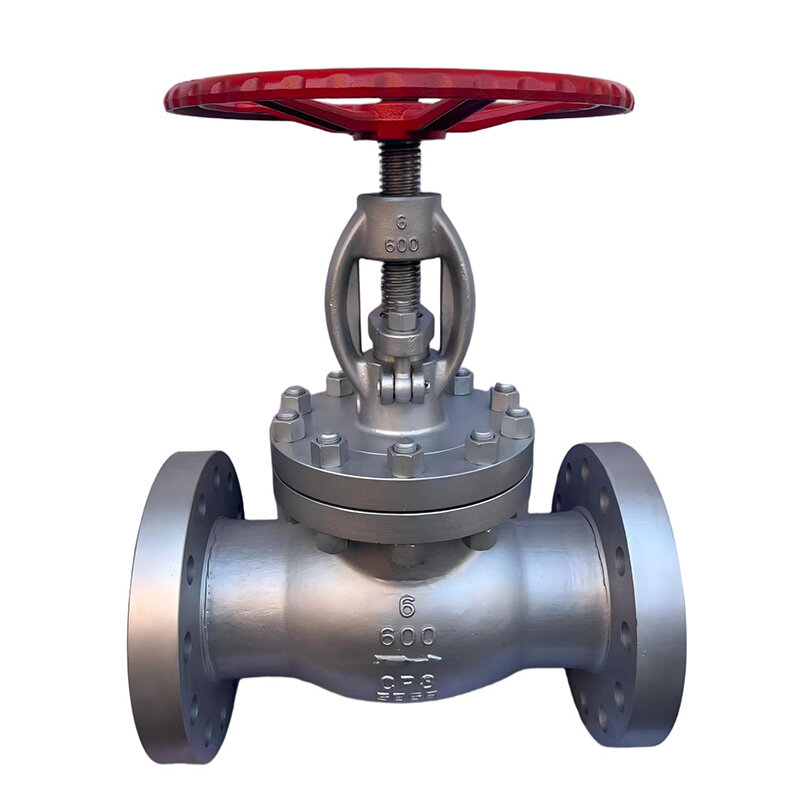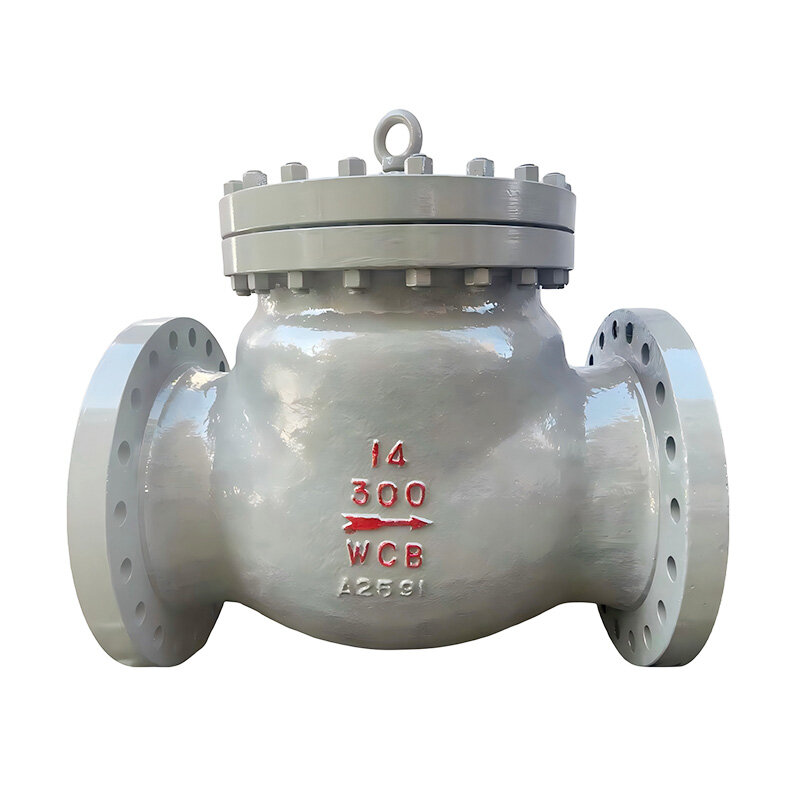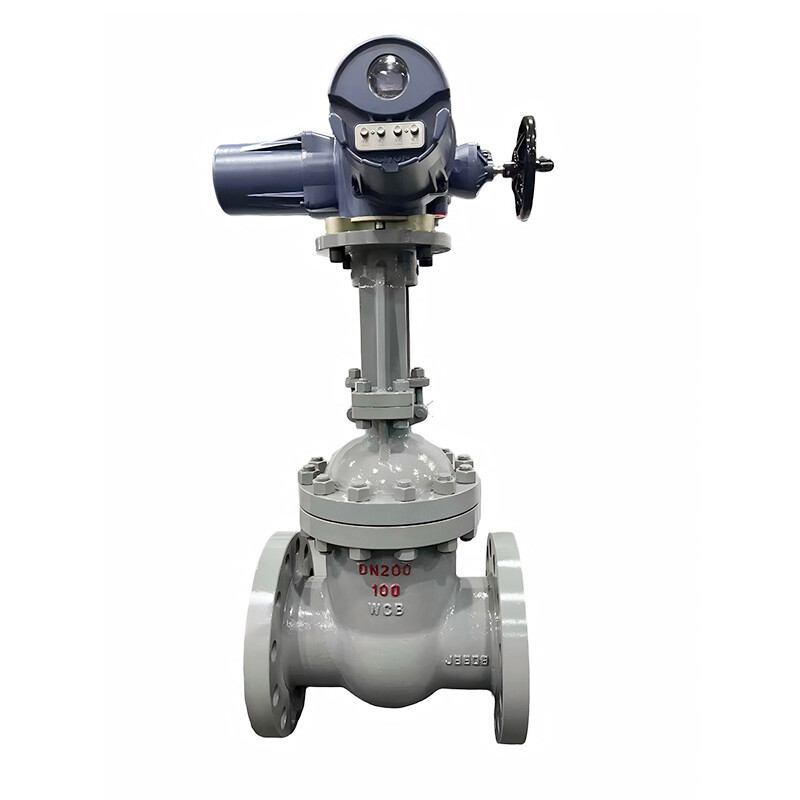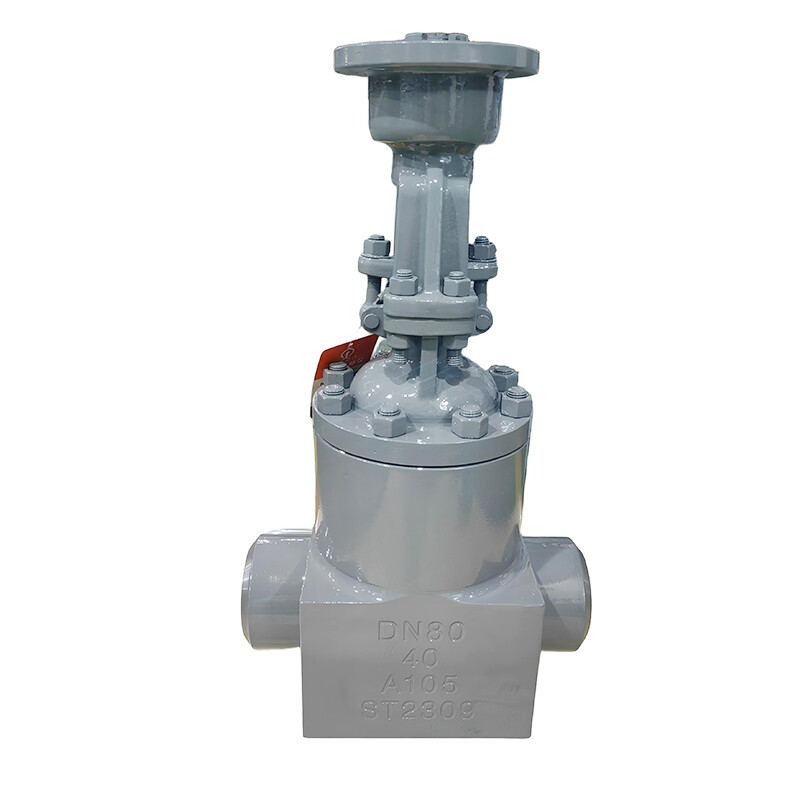
Standard valves often struggle to meet the demands of heavy-duty industrial applications, frequently suffering from issues such as leakage, sticking, and seal failure. In contrast, API globe valves are specifically engineered for rigorous industrial conditions; their superior performance establishes a robust safety barrier for industrial fluid transport, making them core flow-control components in heavy-duty industrial piping networks.
API globe valves are specialized flow-control valves developed specifically for demanding industrial environments. Unlike the generalized designs of standard valves, these products are optimized to address the specific challenges of heavy-duty operations. For high-temperature applications, the valve body structure and sealing materials are optimized to prevent thermal deformation and seal degradation. For high-pressure scenarios, the valve body walls are thickened and the structure reinforced to enhance pressure and impact resistance. To handle corrosive media, corrosion-resistant materials—such as stainless steel and specialized alloys—are employed to withstand acids, alkalis, and sulfur-containing substances, thereby significantly extending the equipment's service life.
In actual operation, API globe valves demonstrate exceptional adaptability. Their unique disc-based throttling structure enables precise flow regulation, making them ideal for applications requiring fine flow control, such as chemical processing and thermal energy management. A stable sealing system ensures zero leakage of high-pressure media, mitigating risks associated with energy loss, environmental pollution, and safety incidents. Smooth opening and closing characteristics effectively dampen the pipeline water hammer effect, protecting auxiliary equipment—such as pumps, instruments, and piping—and reducing the overall failure rate of the network. Furthermore, the valves exhibit excellent fatigue resistance, allowing them to withstand frequent cycling and meet the demands of continuous industrial production.
As safety management in the industrial sector intensifies, the reliability and safety of piping network equipment have become critical considerations in engineering projects. Thanks to rigorous standards, specialized adaptability, and stable operational performance, API globe valves have become the preferred flow-control solution for demanding industrial environments. Whether deployed in onshore heavy-duty piping networks, coastal areas with highly corrosive conditions, or high-temperature, high-pressure thermal systems, these valves ensure long-term, stable operation while significantly reducing maintenance requirements and safety risks. In the future, as industrial operating conditions become increasingly complex, high-performance, customized API globe valves will continue to evolve, safeguarding the safety of industrial fluid transport.