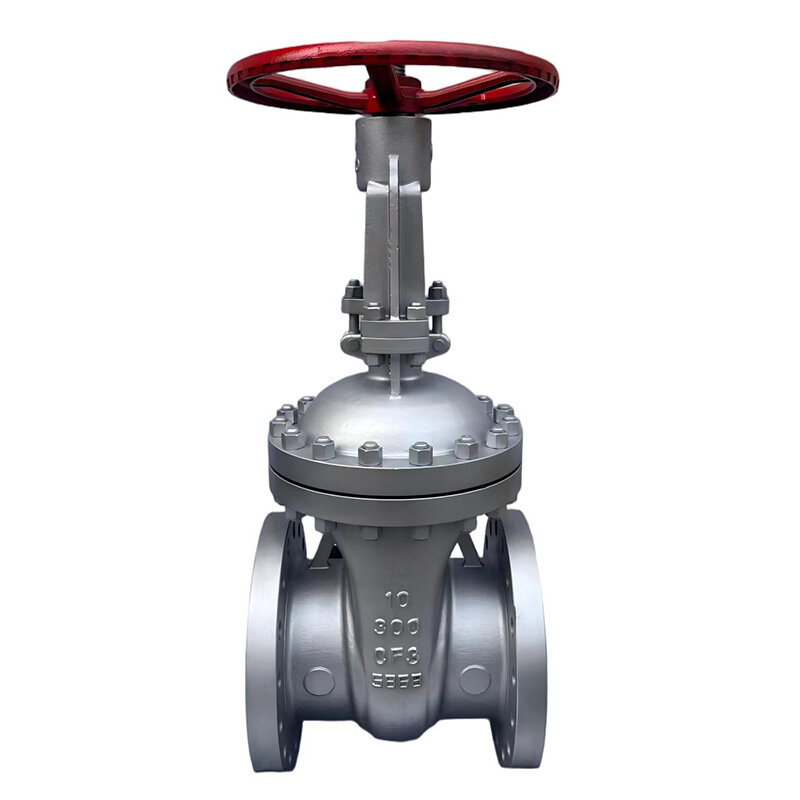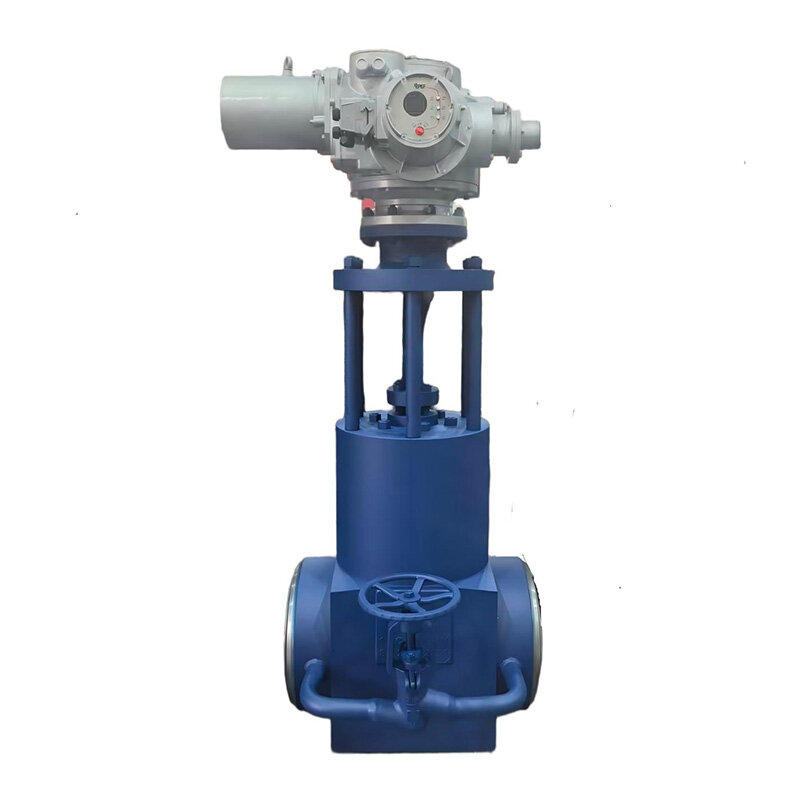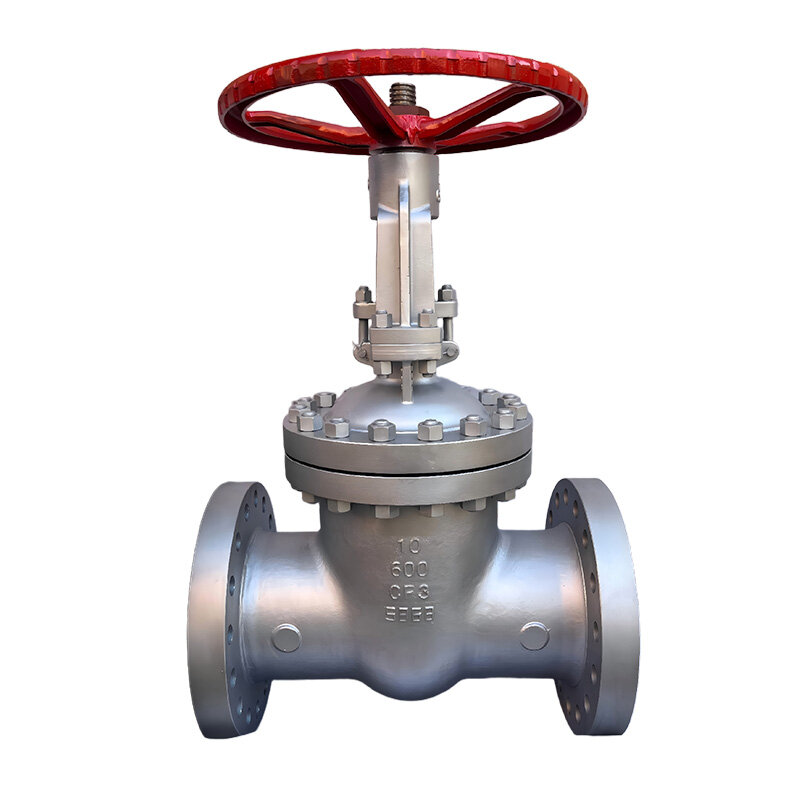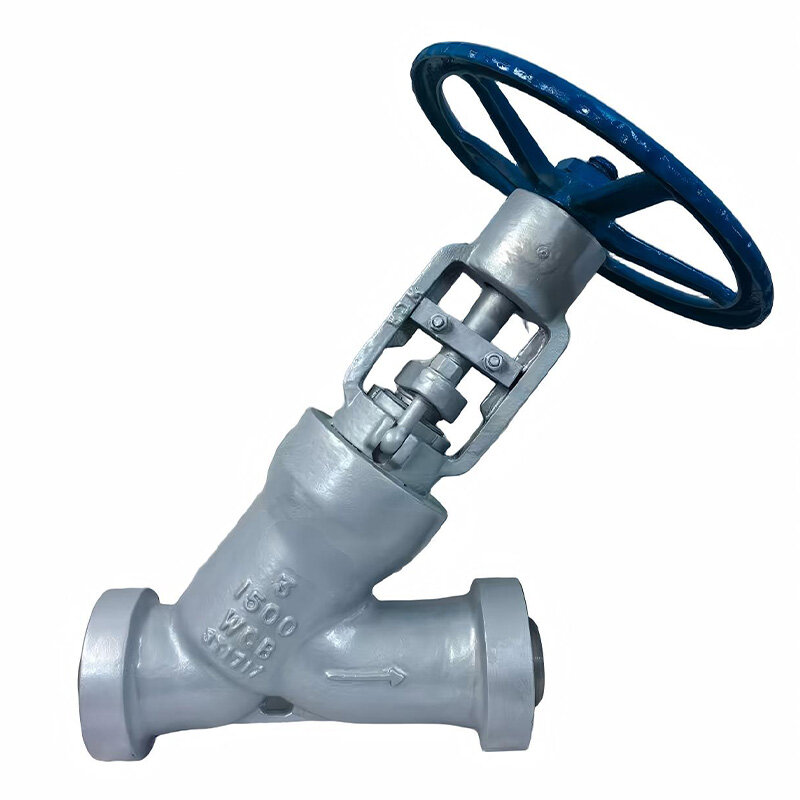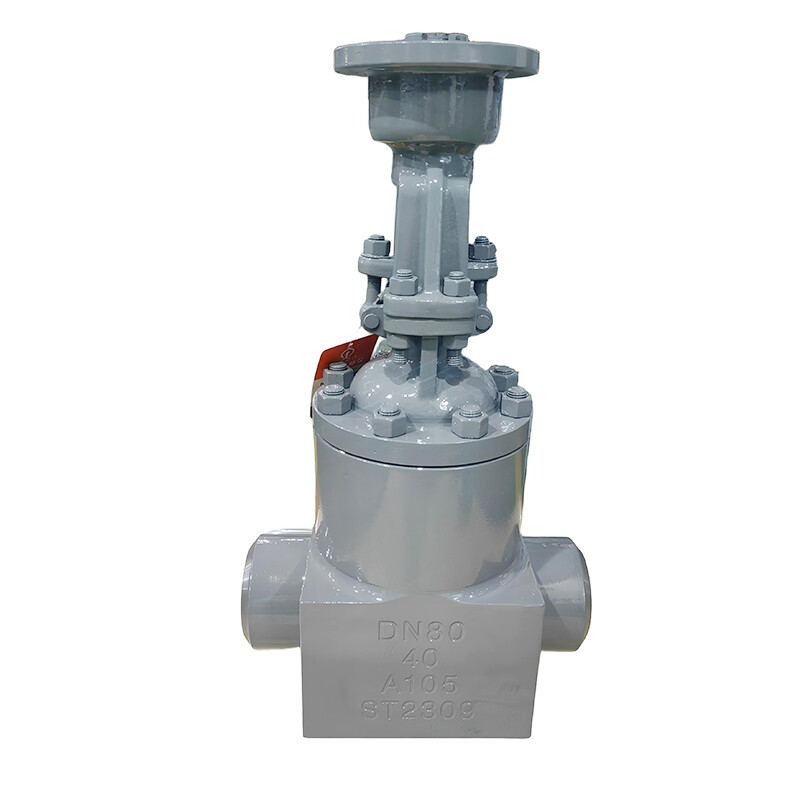
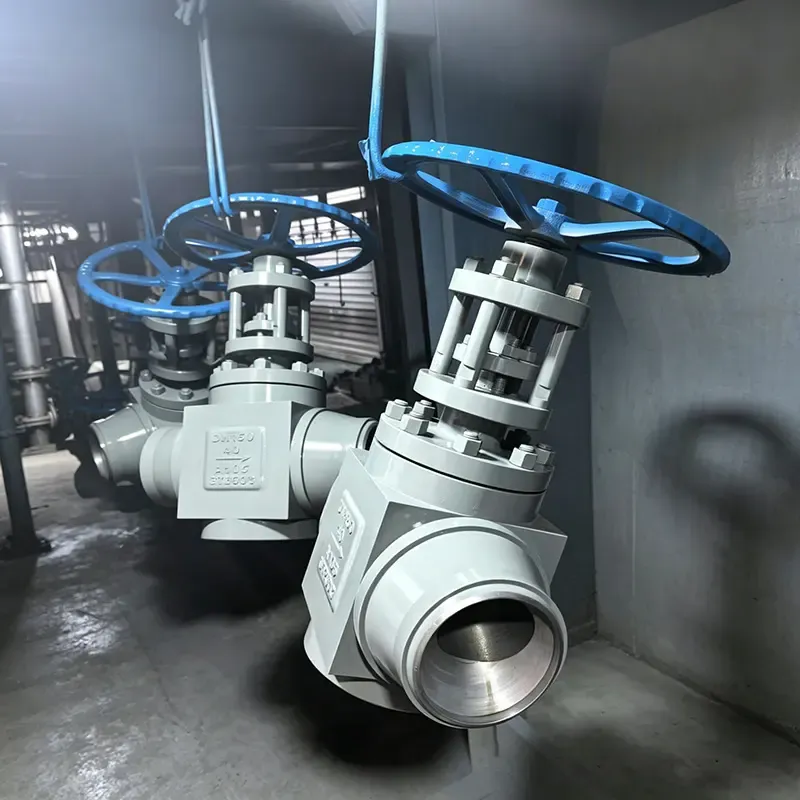
The standardization of industrial valves serves as a crucial foundation for the scaling of industrial systems. Unlike non-standard valves—which often suffer from unstable performance, poor interchangeability, and high maintenance costs—API globe valves have emerged as the benchmark for standardization upgrades. Backed by authoritative standards and featuring universal designs and high performance, they drive the standardization and evolution of fluid control systems across various industries.
The core advantage of API globe valves lies in their rigorous standardized production system; the entire process—from design and material selection to machining and testing—adheres to API industry specifications. Key parameters such as face-to-face dimensions, flange sizes, pressure ratings, and sealing specifications are standardized across the industry, ensuring compatibility with diverse domestic and international piping network designs. Compared to traditional non-standard globe valves, this product resolves industry pain points such as chaotic model designations, replacement difficulties, and inconsistent performance, thereby significantly reducing costs associated with the design, construction, and maintenance of industrial piping networks.
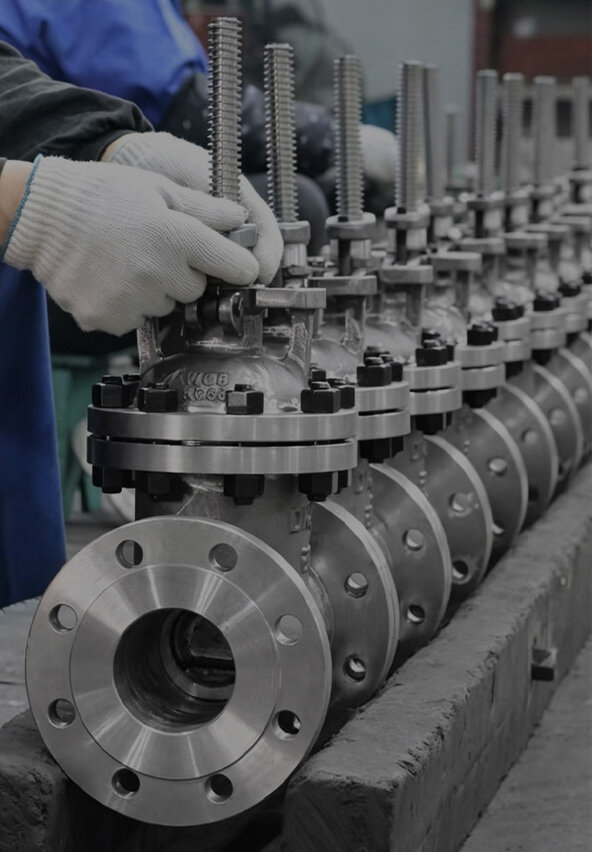
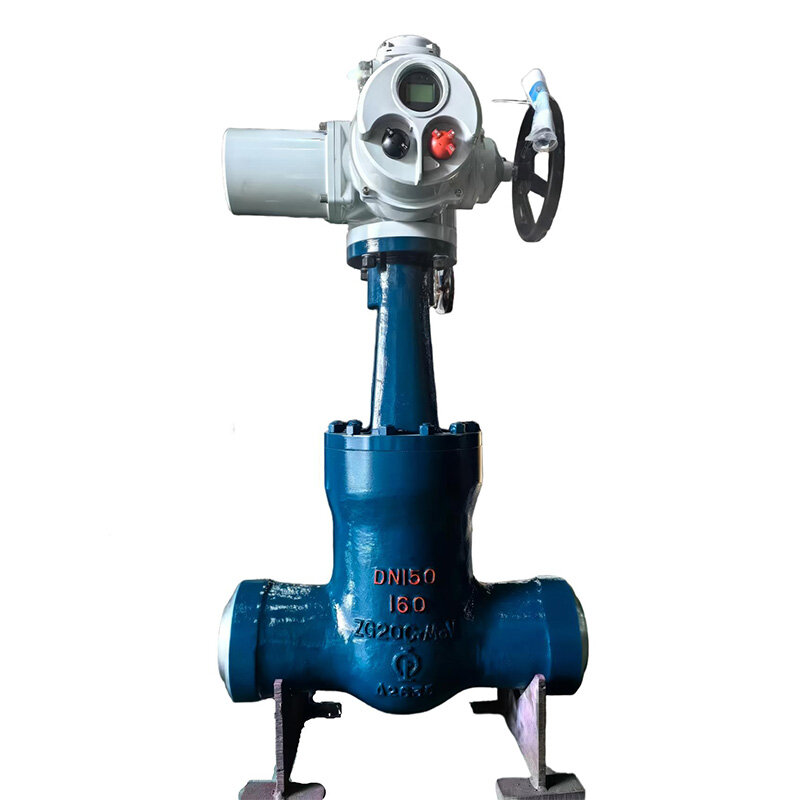
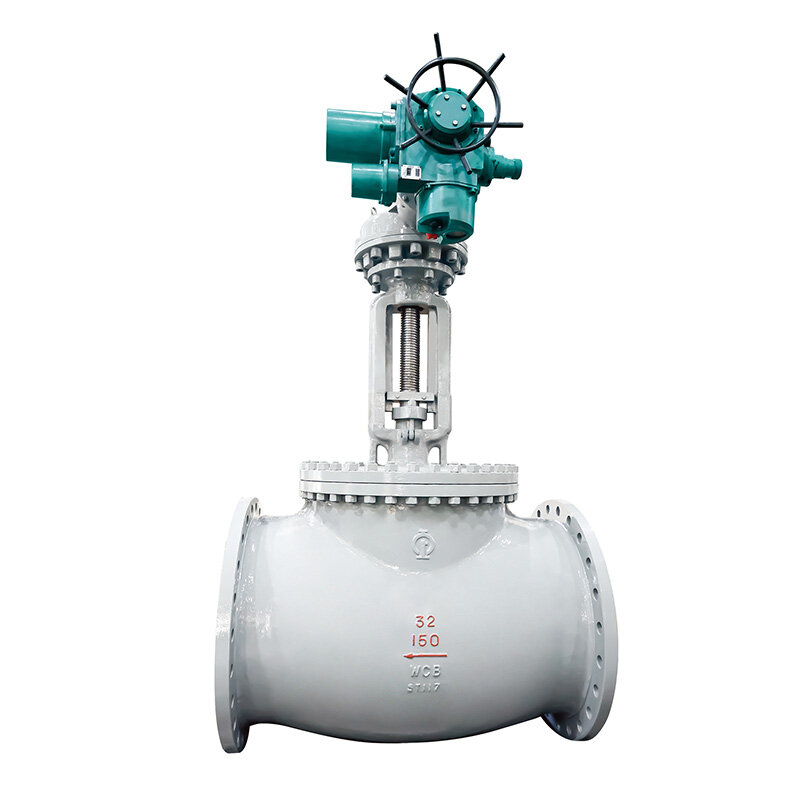
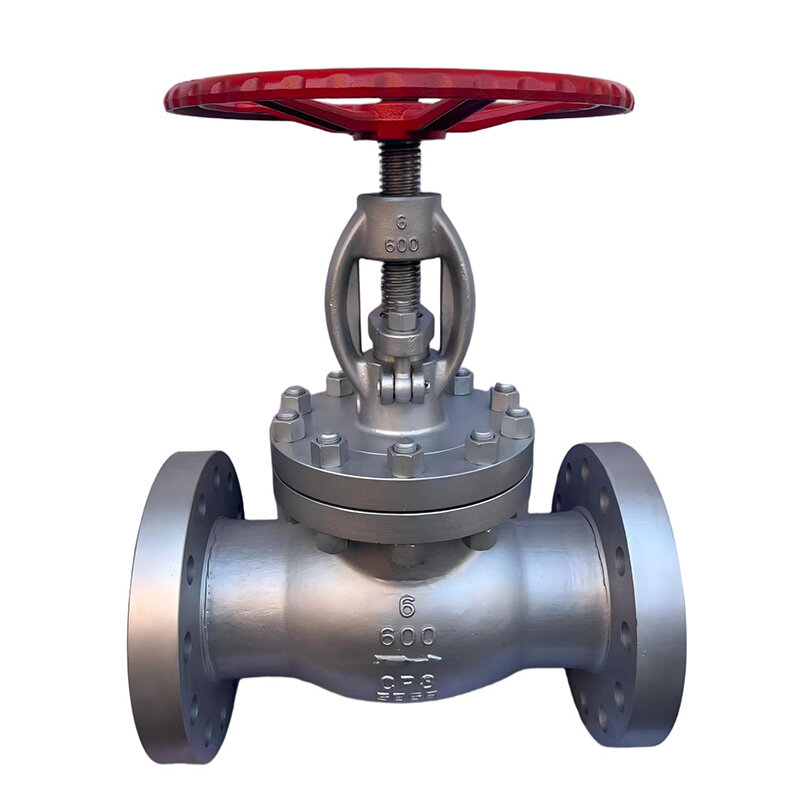
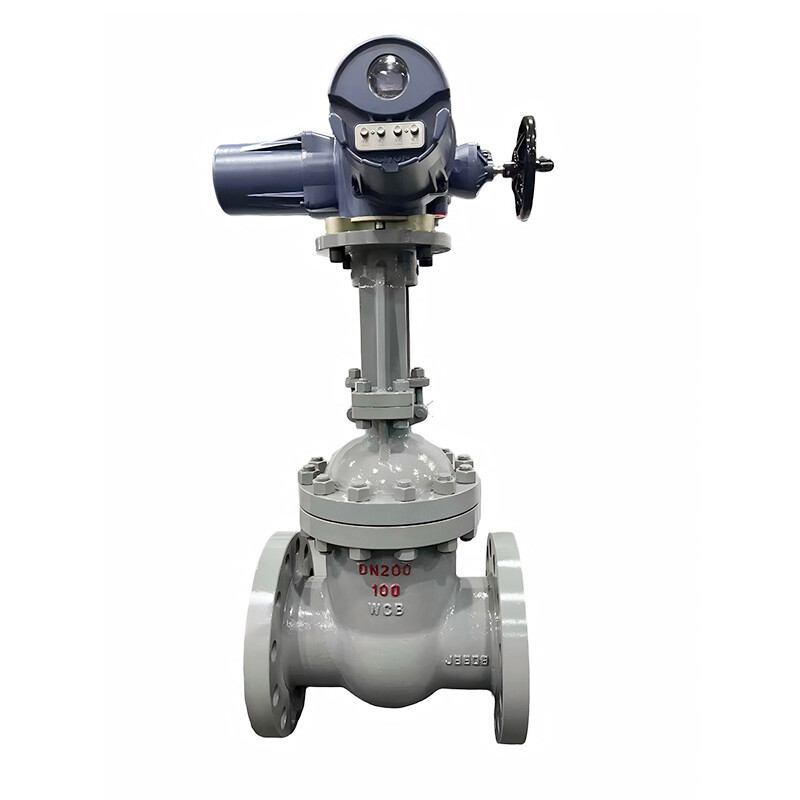
Structurally, API globe valves feature a compact, modular design. They utilize a robust bolted bonnet connection and a tight stuffing box seal, effectively preventing external media leakage even under high-pressure conditions. The valve stem is made of high-strength alloy steel and paired with wear-resistant nuts and bearings, ensuring low operating torque and smooth actuation. Various actuation methods—including manual, electric, and pneumatic options—allow for seamless integration into diverse scenarios such as automated production lines and remote intelligent control systems. Furthermore, the product is certified under API 598 pressure testing standards and offers pressure ratings ranging from Class 150 to Class 1500, meeting the operational requirements of both high- and low-pressure industrial piping networks.
In terms of industrial application, API globe valves serve a wide range of key sectors, including petroleum refining, fine chemicals, thermal power generation, metallurgy, and pharmaceuticals. In continuous chemical production, they ensure stable flow control—enabling precise start-stop operations and fine-tuning—to maintain process continuity. In power and thermal systems, they withstand prolonged exposure to high-temperature, high-pressure steam, ensuring the safe operation of piping networks. In the pharmaceutical and fine chemical industries, stainless steel models meet stringent requirements for transporting clean media, effectively preventing contamination. Currently, the standardization of industrial engineering continues to advance; thanks to their core advantages of versatility, high performance, and high reliability, API globe valves have become the preferred choice for upgrading industrial fluid piping networks, consistently driving the industry's development toward standardization, intelligent operation, and enhanced safety.
Previous:API Globe Valves Empower Chemical Fluid Control
Next:High-performance API globe valves fortify the safety barrier for industrial fluids.