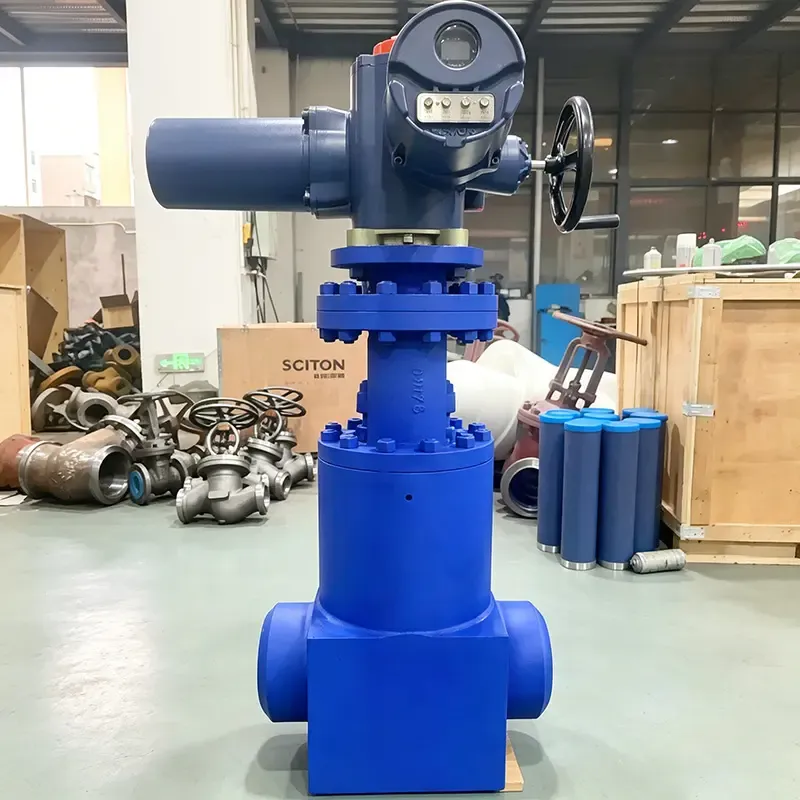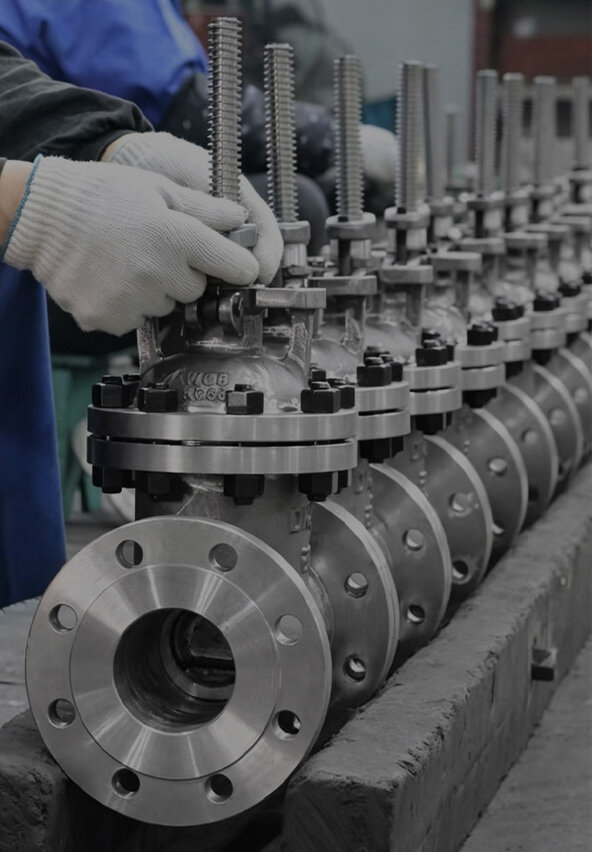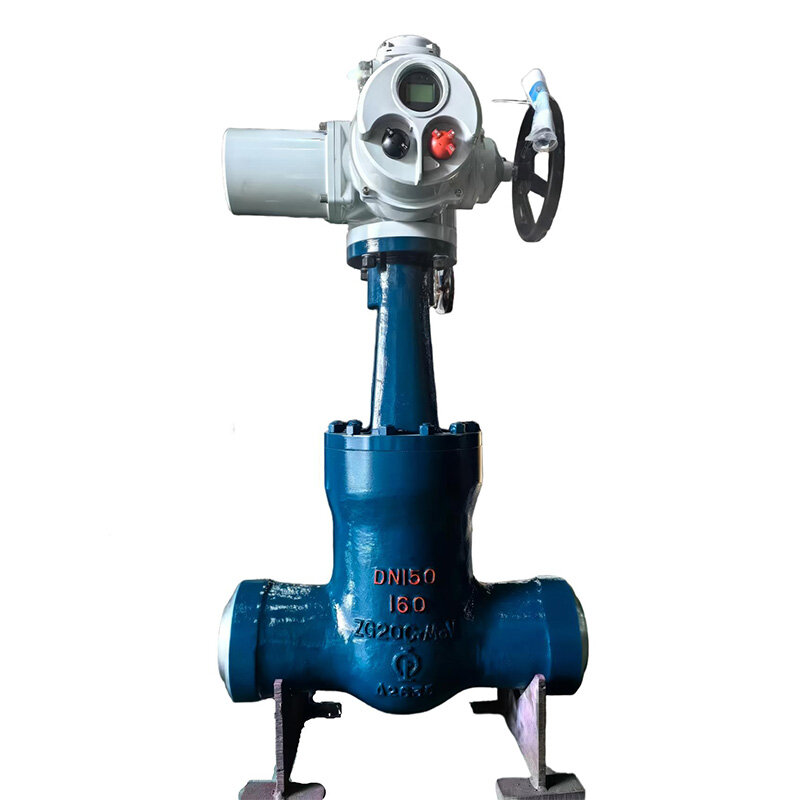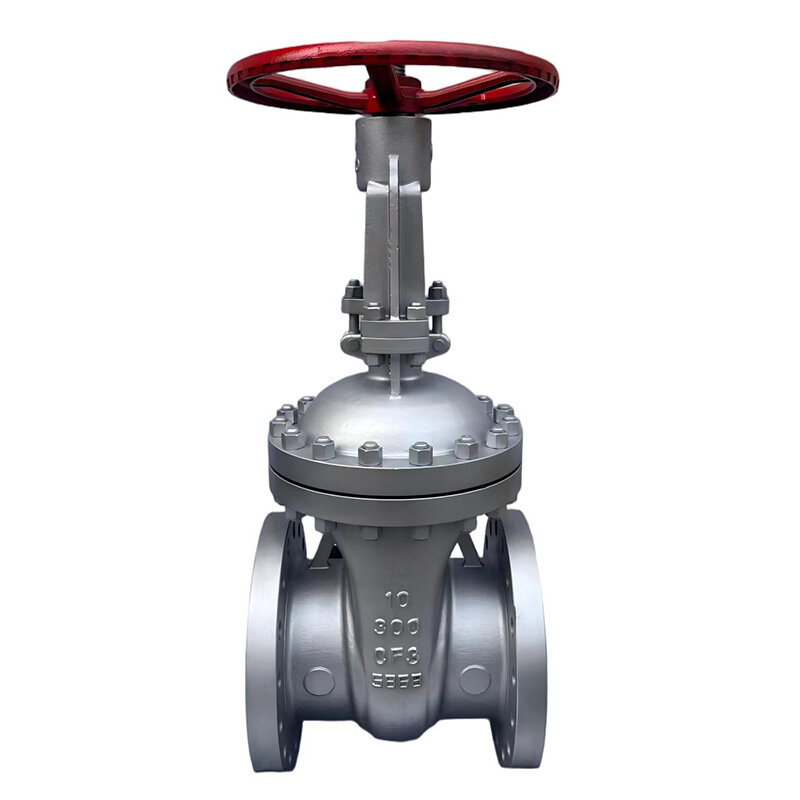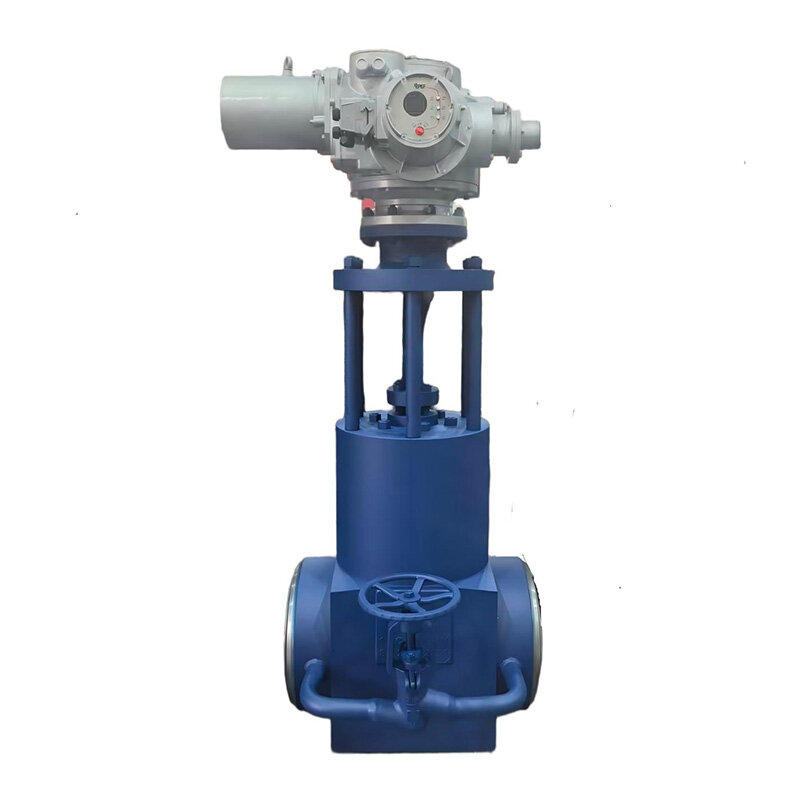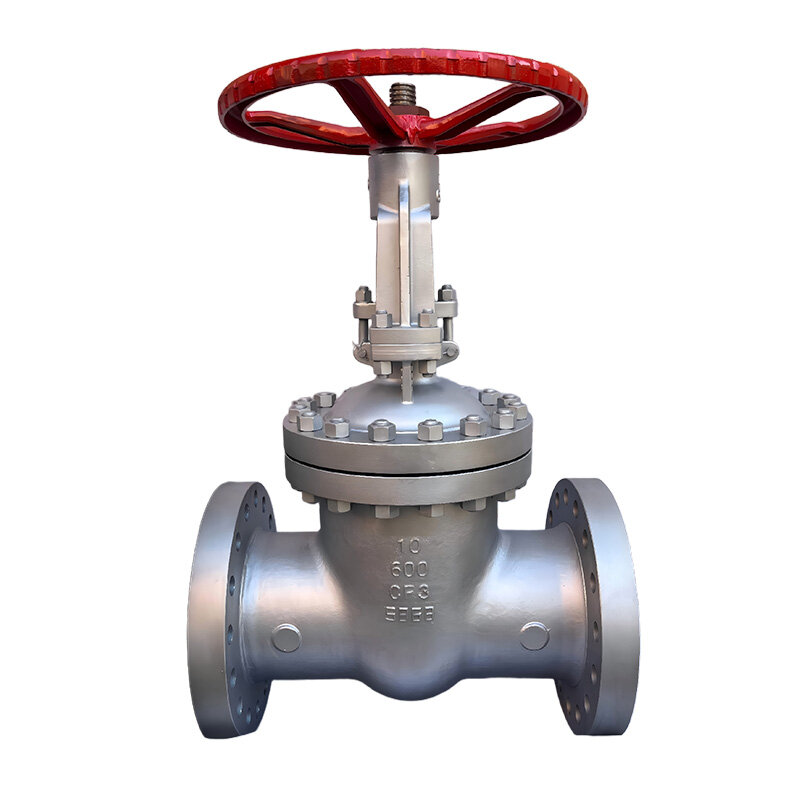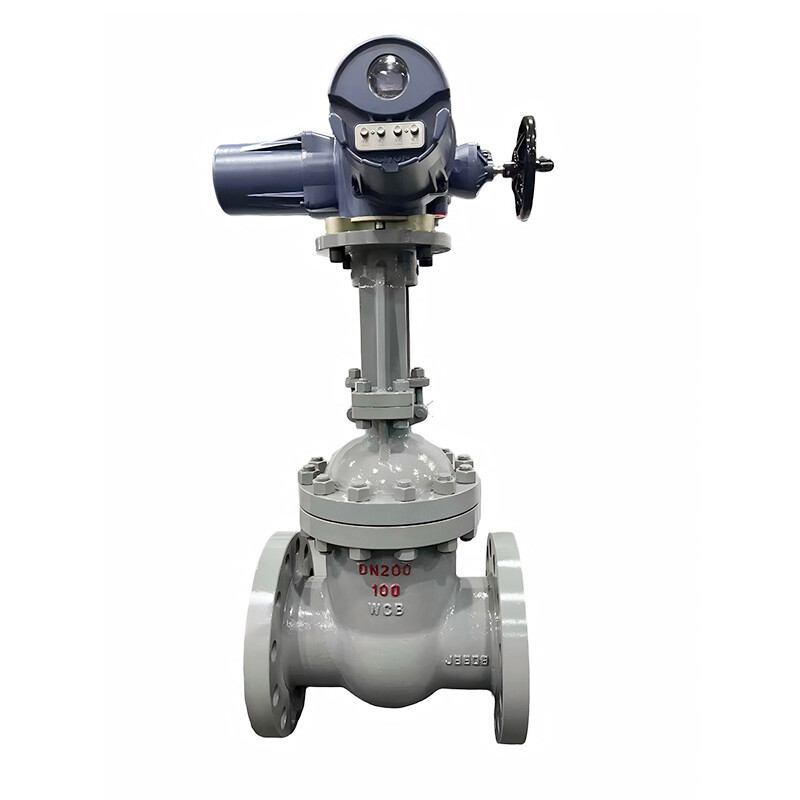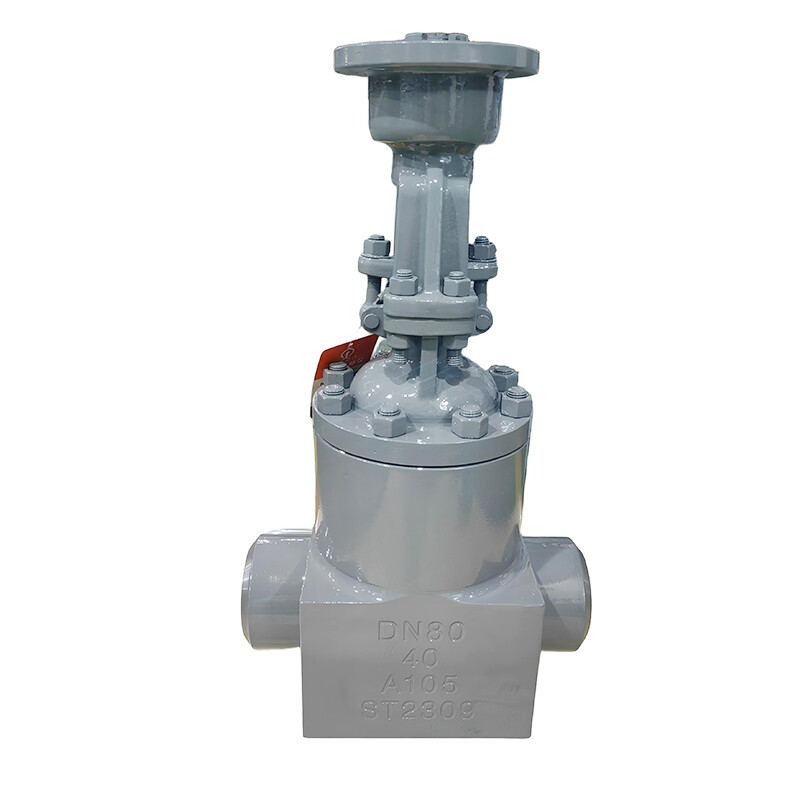
Industrial valves serve as critical control components in fluid transport systems; their standardization and adherence to specifications are fundamental prerequisites for the safe operation of industrial systems. In key sectors such as oil and gas, power generation, and chemicals, API 600 gate valves—backed by authoritative industry standards and proven performance—are increasingly replacing standard non-specified gate valves. They have become the preferred choice for heavy-duty industrial piping networks, facilitating safe and standardized operations and maintenance.
As a standard dedicated to the petroleum industry, API 600 comprehensively covers the entire lifecycle of steel gate valves—from R&D and production to testing. It establishes strict requirements for valve body wall thickness, sealing structures, stem materials, pressure-bearing capacity, and testing methods, thereby fundamentally ensuring product stability and interchangeability. Manufactured in strict accordance with this standard, API 600 gate valves differ from general-purpose gate valves by excelling in suitability for harsh operating conditions and superior safety performance. Utilizing integral forging and precision casting processes, these valves offer high structural strength and exceptional resistance to impact and deformation, ensuring stable, long-term operation in industrial environments characterized by high pressure and frequent cycling.
Regarding sealing performance, API 600 gate valves employ a multi-layered sealing design. The sealing surfaces of the seat and disc feature Stellite hard-facing overlays finished with precision grinding, resulting in high sealing accuracy and wear resistance; this enables them to withstand long-term erosion and corrosion from process media while effectively preventing leakage. Additionally, they are equipped with specialized fire-safe sealing structures that maintain integrity during sudden high-temperature events or fires. Compliance with industrial explosion-proof and fire-safety regulations significantly enhances the emergency safety capabilities of industrial piping networks.
In terms of application, API 600 gate valves are highly versatile, suitable for diverse scenarios ranging from wellhead isolation in oil and gas extraction and shut-off functions in long-distance pipelines to power plant boiler feedwater systems and piping networks handling corrosive chemical media. Whether in the continuous production environments of onshore refining complexes or the harsh marine conditions of offshore platforms, these valves ensure stable operation, substantially reducing equipment failure rates and maintenance costs. Currently, the API 600 standard has been adopted as a key entry-level benchmark for high-end industrial gate valves in industrial engineering tenders and project design specifications, a fact that underscores its industry recognition and practical value.
Amidst the broader industry trends of enhancing quality and efficiency and upgrading safety standards, standardized, high-performance API 600 gate valves will continue to drive high-quality development within the energy and chemical sectors.